China Best Vitamin Gummies Manufacturer for Global Buyers? This question deserves more than a low factory quotation. Global demand is expanding, but buyer expectations are becoming stricter. Fortune Business Insights estimated the global gummy market at approximately USD 21.6 billion in 2023. Its report also projects strong growth through 2032, supported by convenient formats, familiar flavors, and easier consumer acceptance.
The opportunity is visible in small details. A reliable manufacturer should provide batch records, ingredient specifications, stability data, and independent laboratory testing. Buyers should examine pectin or gelatin sources, sugar content, allergen controls, and actual active dosages. Attractive colors are not enough. They cannot replace verified quality.
Duffy MacKay, a senior leader at the Council for Responsible Nutrition, stated, “Supplements are meant to supplement, not replace, a healthy diet.” This principle remains important when developing Vitamin Gummies for international markets. A responsible Chinese supplier should connect formulation experience with transparent documentation, GMP-based production, and consistent export support. Certifications may help, but they do not automatically prove every batch is excellent. That is where buyers must remain careful.
Some claims need restraint. Market forecasts differ by research company, and gummy quality can vary widely between factories. A strong sourcing process should include sample testing, factory audits, and clear acceptance standards before large production begins. The best partner is not always the cheapest one. It is the manufacturer that can explain each ingredient, defend each specification, and improve when something is not right.
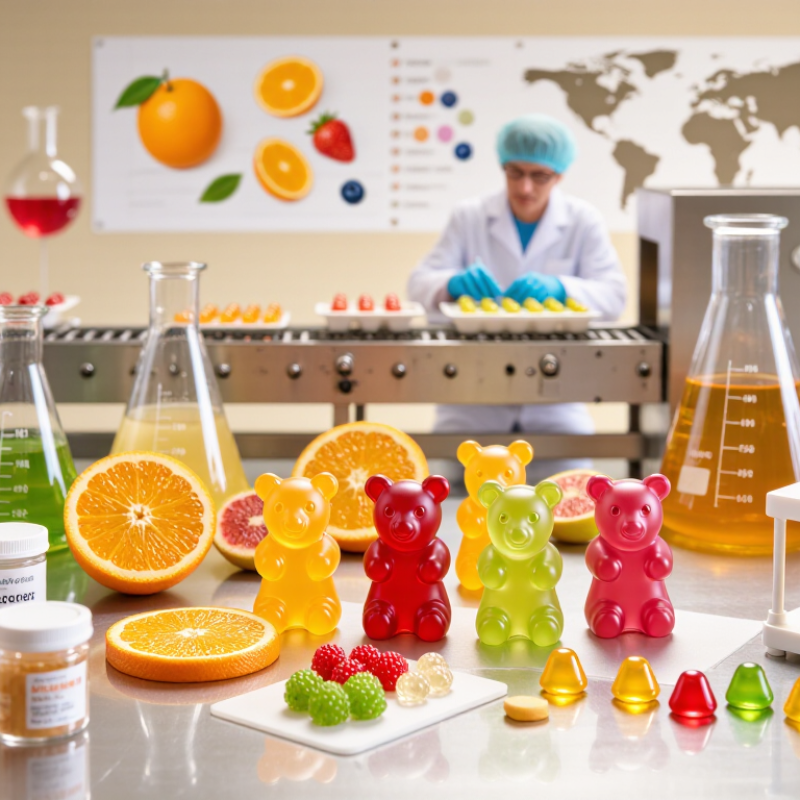
China has become a major vitamin gummies manufacturing center for global buyers. Its strength comes from mature supply chains, skilled production teams, and flexible factory capacity. Many facilities source pectin, vitamins, flavors, and packaging materials through established regional networks.
On a typical production line, operators monitor cooking temperature, moisture, weight, and texture. Small details matter. A slight temperature change can affect a gummy’s shape or shelf stability. Experienced manufacturers use documented procedures, batch records, and controlled production rooms. They can also adjust formulas for different nutritional needs, age groups, and serving sizes.
The advantage also comes from integrated services. One supplier may handle formulation, sampling, testing, packaging, and export documents. This can reduce communication delays and improve batch consistency. Yet speed alone does not prove quality. Buyers should review certificates, laboratory reports, traceability systems, and audit records before placing large orders. A reliable factory explains its testing process clearly. No factory is perfect. A batch may require rechecking when color, texture, or potency falls outside specifications. That honesty matters more than polished promises. From practical experience, steady communication and transparent corrective actions often build stronger partnerships than low pricing.
| Evaluation Dimension | Commonly Available Capability in China | Typical Industry Reference | Value for Global Buyers | Recommended Verification |
|---|---|---|---|---|
| Product format flexibility | Pectin-based, gelatin-based, sugar-free, vegan-positioned, and fruit-flavored gummy formats are commonly offered. | The suitable base depends on dietary requirements, texture, heat stability, and target-market regulations. | Supports different consumer preferences and market positioning without changing the basic delivery format. | Request ingredient declarations, allergen statements, vegan documentation, and finished-product samples. |
| Formula customization | Contract manufacturers commonly support adjustments to active ingredients, flavor, color, shape, serving size, and packaging. | Formula feasibility is affected by active potency, taste, stability, water activity, and the physical limits of a gummy matrix. | Buyers can develop products for children, adults, sports nutrition, beauty, or general wellness applications. | Ask for a formulation brief, stability plan, target dosage, and confirmation of permitted claims in the destination market. |
| Production scale | China has a broad manufacturing base ranging from pilot-scale facilities to high-volume production plants. | Actual capacity varies by line design, batch size, mold configuration, packaging format, and production schedule. | Offers options for market testing as well as larger recurring purchase programs. | Verify monthly capacity, line utilization, batch size, lead time, and production records for comparable products. |
| Ingredient sourcing | Domestic and imported vitamins, minerals, botanical extracts, amino acids, sweeteners, and functional ingredients may be available through established supply chains. | Ingredient quality and legal status must be assessed separately for each destination country. | Multiple sourcing options can support cost, availability, and formula-development objectives. | Request supplier qualification records, specifications, certificates of analysis, and identity or purity testing data. |
| Quality management | Qualified facilities may operate under GMP-based procedures and food-safety systems such as HACCP or ISO 22000. | Certification is facility-specific and does not automatically apply to every product or production line. | A documented quality system helps control raw materials, processing, sanitation, packaging, and release decisions. | Check current certificates, scope, issuing body, audit status, batch records, and corrective-action procedures. |
| Testing and release control | Testing programs may cover microbiology, heavy metals, active-ingredient content, moisture, water activity, and physical appearance. | The required test panel depends on the formulation, raw materials, packaging, and import regulations. | Independent testing and documented release criteria reduce the risk of nonconforming shipments. | Require product-specific certificates of analysis and, where appropriate, reports from an accredited laboratory. |
| Shelf-life development | Gummy products commonly require control of moisture migration, texture, oxidation, color change, and active-ingredient stability. | A shelf-life period should be supported by stability data rather than a generic industry assumption. | Appropriate testing helps maintain product quality throughout transport and storage. | Request real-time or accelerated stability protocols, packaging specifications, and recommended storage conditions. |
| Packaging options | Common options include bottles, jars, pouches, sachets, blister formats, induction seals, desiccants, and child-resistant closures where required. | Packaging selection must consider moisture protection, tamper evidence, transport conditions, and local safety rules. | A broad packaging supply chain can support different price points and retail channels. | Review packaging drawings, material specifications, closure tests, migration documentation, and compatibility results. |
| Private-label support | Many manufacturers can coordinate formula development, label artwork, packaging procurement, filling, coding, and export documentation. | The exact service scope differs between factories, trading companies, and integrated contract manufacturers. | A single coordinated workflow may reduce supplier-management complexity. | Define responsibility for artwork approval, regulatory review, testing, packaging materials, and final product release. |
| Export readiness | Export-oriented suppliers may have experience with commercial invoices, packing lists, certificates of origin, shipping marks, and destination-specific labels. | Import requirements differ by jurisdiction and may include product registration, prior notification, label review, or additional testing. | Familiarity with international documentation can help reduce customs and compliance delays. | Confirm export history for the target market and have an independent regulatory professional review the product before launch. |
| Cost structure | Large ingredient, packaging, equipment, and logistics networks can create competitive cost options, although costs vary by formula and order volume. | The lowest quotation may exclude testing, tooling, packaging development, regulatory review, freight, or quality-inspection expenses. | Buyers can compare total landed cost rather than evaluating unit price alone. | Request an itemized quotation covering formulation, tooling, testing, packaging, inspection, freight, duties, and payment terms. |
Note: Capabilities, certifications, minimum order quantities, lead times, pricing, and regulatory eligibility vary by facility and product. Buyers should verify all claims with current documentation and destination-market requirements.
China Best Vitamin Gummies Manufacturer for Global Buyers?
Choosing a China-based vitamin gummies supplier requires more than checking price lists. Start with production experience, ingredient control, and transparent documentation. Ask how raw materials are tested before entering the factory. Review certificates of analysis, batch records, allergen controls, and finished-product testing. A reliable supplier should explain each step clearly. Vague answers are warning signs.
Visit the facility when possible, or arrange a live video audit. Look at mixing rooms, temperature controls, packaging lines, and storage conditions. Request samples from different batches, not only a polished presentation sample. Check texture, taste consistency, color, seal quality, and label accuracy. Discuss minimum order quantities, lead times, mold fees, and change-control procedures. Compliance requirements differ by market, so confirm claims and labeling with qualified local professionals. No supplier is perfect. A rushed approval can hide small problems that become expensive later.
Tips: Use a written supplier questionnaire. Compare test results with your own laboratory when practical. Ask for a pilot batch before placing a large order. Keep communication records. One overlooked detail, such as gummy moisture after shipping, can affect the entire launch. Experience helps, but careful verification still matters.
For global buyers, vitamin gummy production usually begins with formula review and ingredient verification. Manufacturers check vitamin potency, solubility, taste, allergens, and target-market requirements. Qualified suppliers provide documentation, such as certificates of analysis and traceability records. The formula then moves to a small pilot batch. This step can reveal problems early. A gummy may taste acceptable in theory but feel too sticky after cooling.
The production team heats the syrup base, blends active nutrients, and controls temperature carefully. Excessive heat may reduce the strength of sensitive vitamins. The liquid mixture enters molds, then cools, sets, and dries under controlled conditions. Workers inspect shape, color, weight, and texture. Quality laboratories may test microbial limits, heavy metals, vitamin content, and stability. Packaging follows after approval, with batch codes and storage instructions added for traceability.
Tips: Ask for pilot samples, ingredient specifications, testing reports, and production photographs. Confirm whether the factory controls humidity during drying. Request clear acceptance standards for taste, weight, and appearance. Do not rely only on a polished sample. Actual mass production can vary slightly, especially with natural colors or flavors. A careful supplier explains these limits instead of promising perfect uniformity. Check label compliance for each destination market, because requirements differ. Factory communication also matters. Small misunderstandings about dosage or packaging can become expensive corrections later.
Choosing a vitamin gummies manufacturer in China requires more than comparing prices or colorful samples. Global buyers should verify GMP compliance and a documented food safety system, such as HACCP or ISO 22000. These systems should cover ingredient receiving, cooking, molding, packaging, and sanitation. Ask for recent certificates, audit dates, and the certified facility address. A certificate alone is not enough.
Tips: Request a batch-specific Certificate of Analysis. Check vitamin potency, microbial limits, heavy metals, allergens, moisture, and contaminant results. Confirm that testing comes from an accredited laboratory. Review stability data for the intended shelf life, especially after heat exposure. Also inspect the label proof. Serving size, nutrition values, warnings, and ingredient names must match the destination market.
Traceability is equally important. The manufacturer should connect each finished batch to ingredient lots, production records, and retained samples. Ask whether they can provide a mock recall report. It reveals how quickly problems are identified. During factory reviews, observe handwashing stations, temperature logs, pest controls, and packaging-line separation. Small details matter. I would not rely only on polished factory photographs. Records may look complete, yet an unchecked calculation or weak sampling plan can still create risk. Independent pre-shipment testing adds confidence, although it cannot replace a proper supplier audit.
China Best Vitamin Gummies Manufacturer for Global Buyers?
Global buyers need more than attractive gummies. They need packaging that survives real logistics. Gummies can soften, stick, or lose shape under heat. We usually recommend high-barrier jars, induction seals, tamper-evident closures, and humidity-resistant labels. Desiccants may help, but they must remain physically separated from the product. UNCTAD’s Review of Maritime Transport 2024 reports that over 80% of global merchandise trade by volume moves by sea. That makes carton strength and container planning essential.
Compliance starts before production. A reliable manufacturer should provide ingredient specifications, allergen statements, microbiological results, stability data, and batch traceability. Labels must match the destination market. In the United States, companies are responsible for ensuring supplement safety and truthful labeling. In Europe, permitted ingredients and health claims require separate review under applicable regulations. We have seen projects delayed because one translated claim sounded medicinal. Small wording errors can create large problems. I still believe compliance checklists need human review, not blind automation.
Tips: Request pre-shipment photos, carton drop-test records, and a packing list. Confirm the HS code with your customs adviser. Use temperature indicators for sensitive routes. Ask for retention samples from every batch. Consider an independent inspection. It costs more, sometimes unnecessarily, but one failed shipment costs more. Avoid printing large quantities before label approval. Ensure every certificate shows the matching product name, batch number, and test date.
TO GET STARTED OR FOR A FREE QUOTE CALL 888.454.3466